Original paper: Released original PDF, physical pages62–67.
Nuclear fuel cladding has to retain the nuclear fuel and its fission products, transfer heat to the coolant, and preserve a usable mechanical geometry throughout irradiation. Those functions impose several coupled requirements.
Its neutron absorption cross section should be small: absorption in a structural tube removes neutrons without producing useful fuel fission. This is a major attraction of zirconium alloys in a thermal-spectrum nuclear reactor. Low absorption alone is insufficient, because the material must also tolerate its coolant and irradiation environment.
The tube needs adequate yield strength, fracture toughness and ductility to withstand pressure differences, handling, thermal cycling and fuel expansion. Resistance to material creep and mechanical fatigue limits progressive deformation and cracking. The design must accommodate changes in pressure and contact with the expanding fuel, including pellet-cladding mechanical interaction.
The coolant-facing surface should resist corrosion and loss of protective oxide integrity. Hydrogen uptake and hydrogen embrittlement matter for zirconium alloys; chemical compatibility with the fuel and released fission products matters on the inner surface. Resistance to stress corrosion cracking is particularly important when chemical attack and tensile loading act together.
The material should transfer heat without an excessive temperature drop, retain mechanical integrity at the relevant temperatures, and remain dimensionally acceptable under radiation damage in materials. Irradiation growth, irradiation creep, void swelling and irradiation hardening can alter clearance, stresses and coolant passages even when the unirradiated tube meets its specification.
Finally, the alloy should be manufacturable as thin, reproducible, leak-tight tubing with reliable end joints and inspectable defects. Material selection balances these requirements: increasing strength by alloying, for example, can change corrosion, neutron absorption and irradiation behavior. A high melting point by itself does not establish suitability.
For zirconium alloys, the practical upper temperature is governed by time-dependent corrosion, material creep and loss of ductility, well before bulk melting. In ordinary water-reactor service, cladding surfaces are commonly in the several-hundred-degree range, with normal operation around the low-to-mid range in a pressurized water reactor. A quoted service limit must specify alloy, coolant chemistry, exposure time, stress and accumulated hydrogen; there is no universal temperature at which every zirconium tube abruptly fails.
Increasing temperature accelerates zirconium-steam oxidation and creep. Oxide growth increases thermal resistance, and hydrogen uptake can leave a hydride-containing cladding with reduced resistance to cracking. A transient can also cause ballooning or rupture as hot material loses strength under internal pressure. Oxygen absorbed beneath the oxide stabilizes a brittle oxygen-rich region; a tube that survives the hot part of a transient can still have poor ductility during cooling and quenching.
For scale, the established US emergency-core-cooling criterion discussed by the United States Nuclear Regulatory Commission fuel-damage criteria limits peak cladding temperature to , about , together with an oxidation criterion. This is an accident-analysis criterion, rather than a proposed continuous service temperature.[ref]
United States Nuclear Regulatory Commission fuel-damage criteria. Issue170, description of the10CFR50.46 peak-temperature and17% oxidation criteria
These material constraints limit allowable fuel heat flux and temperature excursions and require adequate heat removal and thermal margin. A small increase in coolant temperature or oxide thermal resistance can raise the underlying metal temperature and accelerate degradation. Alloy changes, protective coatings and alternative claddings aim to improve that margin, while still satisfying the neutronic and mechanical requirements.
The low-temperature zirconium matrix has a hexagonal close packing structure. Its crystallographic and directions therefore have different elasticity, thermal expansion and available slip systems. Producing tubing also develops a crystallographic texture, so averaging over grains does not necessarily remove these directional effects.
Different expansion along the crystal axes produces intergranular thermal stresses during temperature changes. Under load, easy dislocation glide modes may accommodate some strains much more readily than others; additional slip or crystal twinning is needed for general compatibility. Consequently strength and ductility can depend on the axial, circumferential and radial orientation of the tube.
Irradiation creates vacancies and self-interstitials that cluster into dislocation loops with different crystallographic orientations. Their anisotropic accumulation can produce irradiation growth even without external stress. Different directions can elongate or contract while the net volume change remains small. Texture turns these grain-scale strains into macroscopic length and diameter changes, bowing and stresses between constrained components. This mechanism is distinct from the added cavity volume of void swelling.
The crystallographic character of irradiation loops matters: atomistic calculations by Rory Hulse and Christopher P. Race examine several possible loop types and show that loop energy and shape depend on orientation and size. A single generic spherical-defect description therefore misses important aspects of zirconium's dimensional response.[ref]
An atomistic modelling study of the properties of dislocation loops in zirconium by Rory Hulse and Christopher P. Race. Abstract and loop-orientation results; the study is atomistic modelling, not a direct measurement of every loop population
Hydrogen also produces direction-sensitive damage. Zirconium hydrides are brittle precipitates whose preferred orientation depends on crystal texture and stress history. Radially oriented hydrides can offer crack paths across a thin tube wall under circumferential tension. Controlling texture, hydrogen pickup and hydride orientation helps manage that risk; changing the hexagonal structure's orientation cannot by itself eliminate corrosion or irradiation damage.
At low accumulated displacements per atom, a stainless steel can undergo substantial microscopic damage while its macroscopic volume changes little. Irradiation-generated vacancies and self-interstitials recombine, reach defect sinks, or form small clusters and dislocation loops. These processes can harden the steel before a large population of growing cavities appears. Thus dimensional stability during this interval does not imply an undamaged microstructure.
Void swelling commonly has an incubation interval, a transition into appreciable swelling, and a later interval with an approximately steady swelling rate per unit dose. The transition reflects the evolution of both stable cavity nuclei and the competing sink population. Gas atoms can help stabilize small cavities, but a vacancy void need not be filled with high-pressure gas.
The driving imbalance is a vacancy supersaturation. Dislocations generally capture interstitial defects more efficiently than vacancies, giving an interstitial bias. Once stable voids exist, the resulting excess vacancy supply can enlarge them. Growing and evolving dislocation structures compete with the cavities for defects. A roughly steady balance can give an approximately linear volume increase with dose over part of the exposure range, rather than proving indefinite linear growth.
If cavities occupy a fraction of the current volume and the matrix volume is otherwise unchanged, the void swelling volume fraction relation isSince cavity volume scales as radius cubed, numerous tiny clusters and a smaller population of larger voids can have very different dimensional consequences.
The original Cawthorne-Fulton observation of voids in irradiated steel used thin-foil electron microscopy on type316 stainless steel exposed in the Dounreay Fast Reactor. It connected microscopic cavities with the dimensional-instability problem that had emerged during fast-reactor fuel development.[ref]
Voids in irradiated stainless steel by C. Cawthorne and E. J. Fulton. Opening description: irradiated fuel cladding and mechanical-test specimens examined by the thin-foil electron-microscope technique
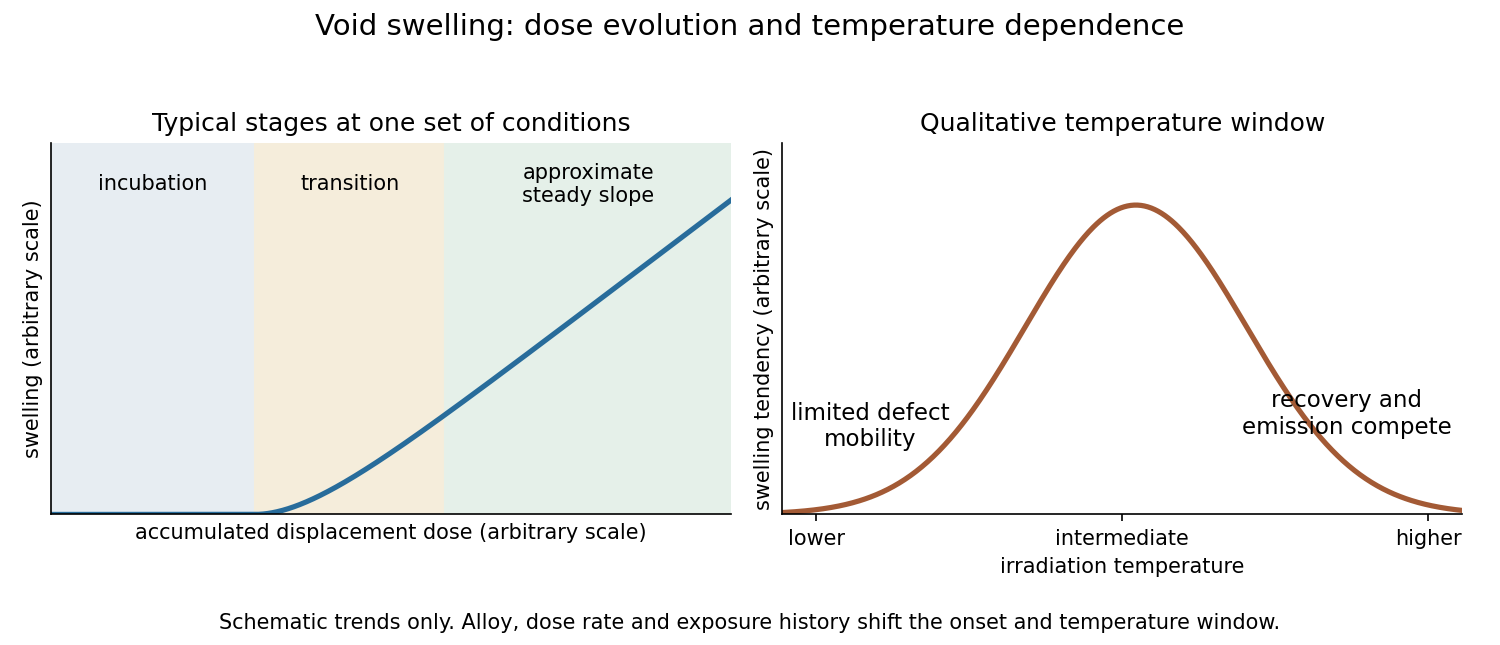
Original schematic of incubation, growing swelling rate and approximate steady swelling; no measured steel data are reproduced
. Details. 
Temperature controls the competition between defect creation, diffusion, recombination, sink absorption and thermal vacancy emission. Consequently void swelling is normally largest in an intermediate temperature window, whose location depends on alloy, dose rate and exposure history.
At low temperature, many generated defects lack sufficient mobility to feed a growing cavity. Considerable irradiation hardening can still occur through small defect clusters, while large-scale void growth remains limited.
At intermediate temperature, vacancies and interstitials migrate sufficiently to establish the biased defect fluxes described above. Cavity nuclei can survive and receive a net vacancy flux, producing strong swelling.
At sufficiently high temperature, thermal vacancy emission, recombination, recovery and changes in sink populations compete more strongly with vacancy absorption. Stable nucleation and net cavity growth can become less favorable. This does not imply that every radiation effect disappears: material creep, precipitation, segregation and gas-bubble evolution can remain important.
For austenitic stainless steels, the relevant range is typically several hundred degrees Celsius; an alloy-independent peak temperature is not justified. Raising the displacement dose rate changes the balance between production and thermally activated processes and can shift both the temperature window and the incubation dose. Temperatures from accelerated ion or electron experiments should therefore be interpreted together with dose rate, implantation, specimen thickness and surface-sink effects.
Reducing void swelling means delaying stable cavity growth and reducing its rate after incubation. Several approaches act on different parts of that mechanism.
Choose an alloy and initial microstructure with favorable defect sink populations. Grain boundaries, stable interfaces, precipitates and a controlled dislocation structure can remove mobile defects and promote recombination before they feed voids. The relevant quantity is sink efficiency and bias, rather than the number of visible microstructural features alone.
Cold working can increase the starting dislocation density and prolong incubation in suitable austenitic steels. Irradiation and thermal recovery can later change that structure, so an initial benefit need not persist indefinitely. Solute additions and controlled precipitation can also change vacancy mobility, defect trapping and cavity nucleation. Their effectiveness must be assessed together with corrosion, ductility and irradiation-assisted changes in composition.
Where other constraints permit, choose a more swelling-resistant material family, such as an appropriate ferritic-martensitic steel, rather than assuming every stainless steel has the response of an austenitic grade. This introduces its own tradeoffs in toughness, temperature window and compatibility.
Manage the operating temperature and accumulated dose to avoid the most unfavorable swelling regime, and account for transmutation-gas production. Neither simply minimizing temperature nor adding gas traps guarantees an improved component: the former can increase hardening and embrittlement, and gas-stabilized cavities can become nuclei for later swelling.
Useful comparisons require specimens with controlled composition and heat treatment, measured dose and temperature histories, and both dimensional measurements and transmission electron microscopy. Matching final dose alone does not establish that two irradiation conditions produce the same swelling.
An energetic neutron can collide with a lattice atom and create a primary knock-on atom. That recoil transfers energy to other atoms in a displacement cascade. Some atoms leave their normal lattice sites, creating Frenkel pairs: a vacancy and an extra atom at an interstitial position.
Many nearby defects recombine during the cascade and its thermal relaxation. The surviving point defects are therefore fewer than a simple count of all displacement events. Some defects are already clustered within the cascade; others migrate and aggregate later.
A collection of vacancies can collapse into a platelet bounded by a vacancy-type dislocation loop. An aggregation of self-interstitial atoms can create an extra atomic platelet bounded by an interstitial-type dislocation loop. The boundary is a line defect because a circuit around it has a nonzero Burgers vector. The allowed Burgers vectors and habit planes depend on the material's crystal structure and fault energies.
Loops can grow by absorbing mobile point defects, shrink by emitting or absorbing the opposite defect type, and interact with existing dislocations. Some remain faulted, while suitable loops can unfault or become part of a larger dislocation network. Repeated cascades and subsequent defect transport therefore create a population of extended defects even in material with a low initial dislocation density.
This describes the main displacement-damage mechanism. Ionizing energy deposited in a material does not automatically create the same defect population as a neutron recoil cascade; recoil spectrum, displacement thresholds and material response matter.
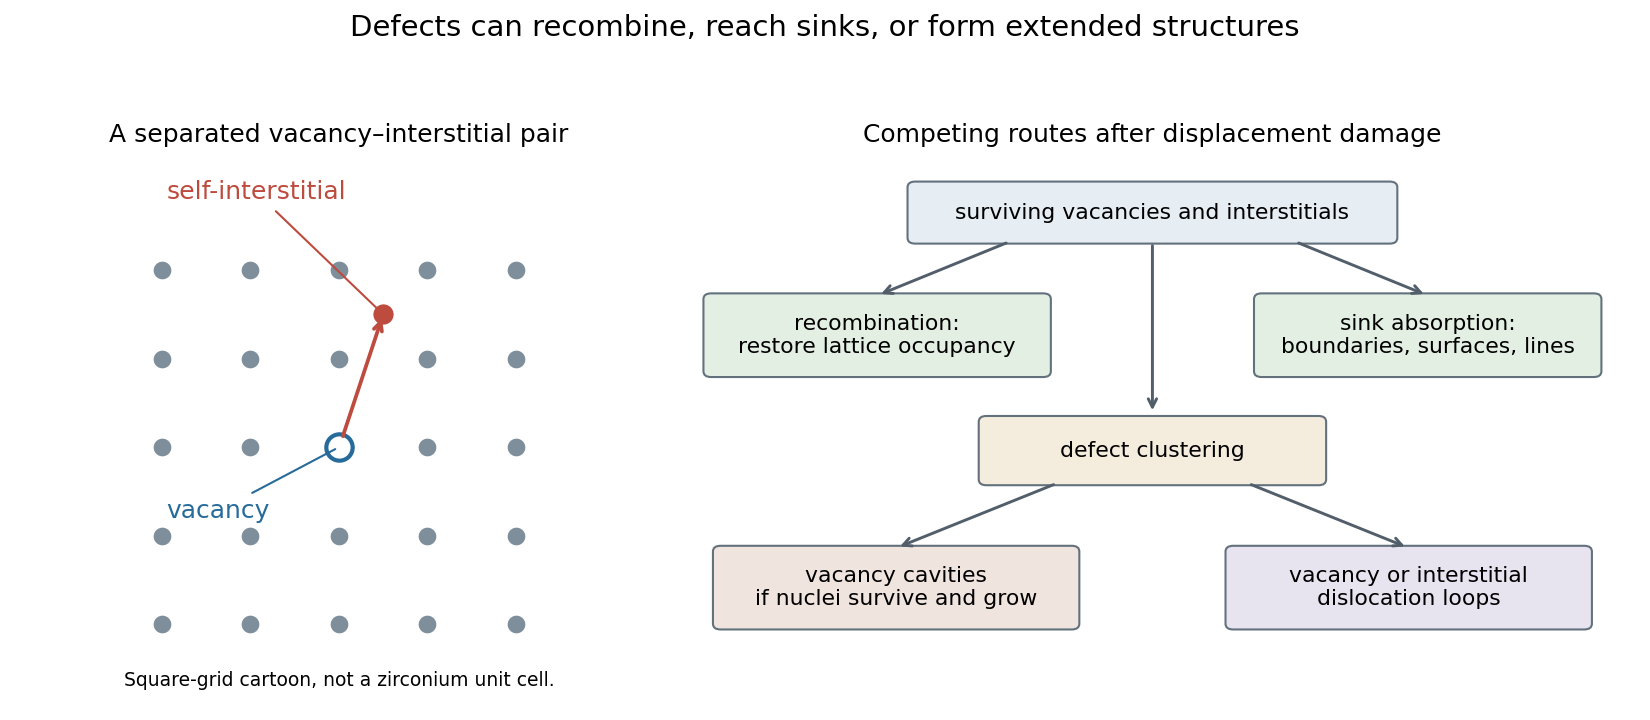
Original schematic of a displaced atom, a Frenkel pair, and the competing pathways to recombination, sinks, loops and voids
. Details. 
The resulting dislocation density reflects competing production, growth and recovery rates. The irradiation spectrum and displacement dose rate set the supply of recoil cascades and surviving point defects. Cascade structure controls the fraction born as isolated defects or clusters; equal nominal displacements per atom can therefore give different defect populations.
Temperature sets vacancy and interstitial mobilities and the rates of thermal emission and recovery. A simple radiation damage rate theory model illustrates the competition using number densities :Here is the surviving mobile-pair production rate per volume, is the recombination coefficient, are diffusion coefficients, and are sink strengths. The model omits explicit cluster-size populations and thermal-equilibrium emission; those must be added for a quantitative description of a particular exposure.
The initial dislocation density, grain size, free surfaces, precipitates and existing cavities all change sink strengths. Dislocations can have an interstitial bias, so their capture rates for the two defect types differ. Solutes and transmutation gases alter defect binding and mobility. Crystal structure, elastic anisotropy and applied stress affect which loop orientations survive and grow.
For a number density of circular loops of radius , their contribution to line length per volume isThus loop nucleation and loop growth both increase dislocation density, while shrinkage, annihilation and absorption at other sinks can decrease it. A change in loop count alone does not determine the change in total line density.
Schematically, is a production-and-growth contribution minus recovery and annihilation. An initial rise followed by approximate saturation is possible when these balance, but the saturation value and approach rate depend on the evolving microstructure. There is no universal dislocation density fixed by dose alone.
Mixed oxide fuel begins as a specified mixture of uranium and plutonium oxides. A fuel pin develops strong radial temperature gradients during operation. The components and oxygen need not remain spatially uniform: their chemical potentials depend on temperature, local composition and oxygen-to-metal ratio.
Actinide redistribution in oxide fuel can involve thermally driven solid-state diffusion and evaporation–condensation transport across pores or a central cavity. Oxygen redistributes as well, changing local oxidation states and the relative thermodynamic tendencies of uranium- and plutonium-bearing species. Pore migration, grain growth and central-void formation couple compositional redistribution to fuel restructuring. Differential local burnup also changes composition over time.
The direction and magnitude of plutonium migration cannot be inferred from a temperature gradient alone. In particular irradiated fast-reactor pins, enrichment around a central cavity has been observed, but the result depends on stoichiometry and operating history. M. Bober and colleagues investigated thermal-diffusion and evaporation–condensation effects using autoradiographs of sections of fuel irradiated in RAPSODIE.[ref]
Plutonium redistribution in fast reactor mixed oxide fuel pins by M. Bober and others. Abstract: irradiated-pin autoradiographs, oxygen redistribution, and dependence on stoichiometric state
Redistribution changes the radial heat generation rate and material properties. Concentrating more fissile material near an already hot region can raise local heat generation; changes in thermal conductivity and local melting behavior modify the temperature response. Gas release, pore formation and fuel–cladding contact can also change thermal resistance and mechanical loading. A spatially averaged composition can therefore underestimate a local temperature or chemical interaction.
Segregated fission products add another concern: mobile species can accumulate at colder interfaces or react with the cladding, while insoluble products form separate phases. Fuel performance must therefore track composition, temperature and microstructure together, rather than treating segregation as merely a cosmetic change in an otherwise fixed fuel.
Mitigation should reduce the driving gradients and keep the resulting material response within a demonstrated range. A uniform starting mixture and controlled pore and grain structure reduce pre-existing local compositional and thermal variations. Control of the oxygen-to-metal ratio matters because oxygen chemistry changes both transport and fuel–cladding compatibility.
Reducing peak temperature and unnecessary thermal gradients limits thermally activated redistribution and evaporation–condensation. Possible design responses include improving heat transfer, choosing suitable fuel geometry and thermal properties, and limiting local power peaking. Their benefit has to be checked against neutronic performance, mechanical constraints and changing properties during burnup.
Materials selection and interface design can reduce harmful fuel–cladding chemical interaction. Retaining a suitable gap, limiting cladding attack and accommodating gas and swelling are coupled requirements; simply suppressing one transport pathway can leave other degradation mechanisms.
Finally, use post-irradiation composition profiles and microstructural examinations to test the fuel-performance model. Measurements at different radii and axial positions can reveal whether an assumed homogeneous composition remains adequate. An observed redistribution in one fuel history does not establish a universal correction for all mixed oxide fuel. Mitigation aims at acceptable temperature, integrity and lifetime, rather than promising that every atom remains at its original radial position.
For the 2021 context, candidate improvements include modified oxide fuels and several higher-density or higher-conductivity alternatives. Their attraction and limitations should be stated together.
Doped uranium dioxide aims to improve the microstructure and behavior of a familiar oxide fuel. Controlled dopants and larger grains can change gas retention, creep and cracking. This preserves much of the oxide-fuel experience while still requiring qualification of the modified material.
Uranium silicide and uranium nitride offer high uranium loading and potentially improved thermal conductivity, which can reduce the temperature rise needed to remove a given power. Their chemical compatibility with water, irradiation stability, swelling and fission-gas behavior require assessment; a favorable fresh-fuel conductivity alone does not establish a better fuel system.
TRISO fuel uses multiple coating layers around small fuel kernels to retain fission products, particularly for high-temperature gas-cooled systems. Coating integrity, irradiation effects and heat transfer through the coated-particle compact remain central requirements. It is a different fuel architecture, rather than a simple drop-in replacement for every water-reactor pin.
The contemporary accident-tolerant fuel program also studied combinations such as doped oxide or silicide pellets with chromium-coated zirconium cladding, and silicon-carbide cladding concepts. The fuel and cladding improvements act on different failure mechanisms and must be qualified as a coupled system.[ref]
Accident-tolerant fuel development awards by the United States Department of Energy. 2019 program announcement, development plans through2021: doped oxide, silicide and alternative cladding concepts
The common aim is improved retention and thermal/mechanical performance under normal and off-normal conditions while preserving acceptable neutronics, coolant compatibility, manufacturability and end-of-life behavior. No candidate is superior on every property, and the question supplies no basis for declaring one universally optimal.
Articles by others on the same topic
There are currently no matching articles.